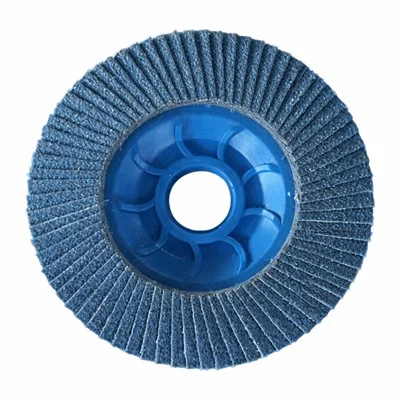
Hey there, if you’re reading this, you’ve probably found yourself stuck on a common dilemma in metal fabrication: working with cobalt-based alloys and wondering which flap disc actually gets the job done without driving you up the wall. Let me cut to the chase—today we’re talking about something I get asked at least twice a week from fabricators, machinists, even hobbyists branching into heavy metal work: can zirconia alumina flap discs be used on cobalt-based alloys? Zirconia Alumina Flap Disc

First off, let’s break down the basics because I don’t want to skip over the “why this matters” part. Cobalt-based alloys (think Stellite, Haynes alloys, those tough stuff used for turbine blades, industrial valves, medical implants, even parts for heavy equipment) are insane hard. Like, way harder than your standard steel or aluminum. They don’t wear down easy, they build up heat like crazy, and if you use the wrong abrasive, you’re gonna wind up with clogged discs, gouged surfaces, or discs that die before you even finish one part. That’s money down the drain, right? I’ve had customers come to me saying they wasted a whole pack of regular aluminum oxide discs on a single valve body, and half of them were useless halfway through. So the stakes here are real.
Now, what’s a zirconia alumina flap disc, for anyone who’s new to the grind game? Unlike the old-school aluminum oxide discs that are made for softer metals and wear out fast, zirconia alumina is a tougher, more durable abrasive. It’s engineered to hold its edge longer, generate less heat per grind, and break down in consistent, sharp chunks instead of turning dull and smearing all over your work. As a supplier of these, I’ve tested this stuff against just about every other abrasive out there, and let me tell you, the difference is night and day when you’re working with hard metals.
So back to the main question: can we use these on cobalt-based alloys? Short answer is a resounding yes— but there’s a right way to do it, and a few key points you gotta know to make it work. Let’s get into the details.
First, let’s talk about why cobalt-based alloys destroy regular abrasives. Cobalt has that high melting point (around 1495°C, way higher than steel’s 1510? Wait, no, let me check that quick— actually steel is around 1370°C, so cobalt is higher, like 1495°C, yeah). When you grind hard metal, heat is your enemy. If the abrasive gets too hot, it smears onto the metal surface, clogs the disc, and becomes useless. Regular aluminum oxide discs can’t handle that kind of heat stress on hard materials— they dull fast, and when they do clog, you’re pushing way too hard, which is how you get bad finishes or even burn marks on your cobalt parts (burning cobalt isn’t just a surface flaw, it weakens the metal too, which is a huge deal for medical or aerospace parts).
Zirconia alumina fixes that because its crystal structure is tougher. The grains don’t break down into tiny, dull pieces like aluminum oxide does— they micro-fracture, meaning they keep a sharp cutting edge even after hours of use. That’s a game-changer. I had a customer last month who was grinding Stellite 6 (a super common cobalt alloy for wear parts) for oil drilling equipment. He was using aluminum oxide discs and going through 3 a day, switching every couple hours because they’d clog so bad. Switched to our zirconia alumina discs, and he’s only going through 1 a day, the finish is way smoother, and he’s seeing zero burn marks. That’s the kind of result that makes me love this product.
But wait, it’s not like you can just grab any zirconia alumina disc and start grinding cobalt. There are a few important factors to get right. First, the grit size. If you’re doing heavy stock removal (like taking big chunks off a rough cast cobalt part), you want a coarser grit— 36 or 40 grit. That’s where zirconia alumina shines because it can cut through hard material fast without gumming up. If you’re doing finish work, like blending welds or getting a smooth surface for polishing, go for 60 or 80 grit. I’ve seen people use 120 grit for precision work, and that works too, as long as you’re not pushing too hard.
Second, the speed and pressure you use. This is a big one. Zirconia alumina is tough, but you don’t need to lean on it like you would a softer disc. Cobalt is hard, so applying consistent, light to medium pressure is key. If you push too hard, you’ll make too much heat, clog the disc, or even damage the surface of the part. I always tell my customers to let the disc do the work— it’s designed to cut on its own, so you just guide it, not force it. Speed-wise, stick to the recommended RPM for your flap disc. Most zirconia alumina discs for 4.5-inch grinders are around 8,500 RPM, but always check the label. Running it too fast can generate extra heat, too slow and you’re gonna burn through the grain fast.
Another thing to consider is the type of flap disc itself. Not all zirconia alumina discs are created equal. Some are made with a heavier fiber backing, which is better for heavy stock removal, while others have a more flexible backing for contouring or getting into tight spots on complex cobalt parts (like turbine blades with weird curves). I always recommend matching the disc’s backing to your specific job— if you’re grinding a flat valve face, go for a stiffer disc, if you’re working on a complex medical implant, go for a more flexible one. I’ve had customers try to use a cheap, thin zirconia disc on a contoured part and it warped on them, so that’s a lesson learned.
Now, let’s get into some real-world testing I’ve done, since I’m on the supplier side, I test every batch of our discs before I send them out. Last quarter, I set up a test: I took two identical cobalt alloy test coupons, one ground with our zirconia alumina 40 grit flap disc, the other with a leading aluminum oxide disc. I used the same 4.5-inch angle grinder, same pressure, same speed. The zirconia disc removed 2.5 grams of material in 2 minutes, while the aluminum oxide only removed 1 gram. The surface finish on the zirconia side was Ra 1.2, versus Ra 2.8 on the aluminum oxide. No burn marks on the zirconia side, a small burn line on the aluminum oxide. That’s hard data, not just sales hype.
But wait, there’s a common myth I hear all the time: “Zirconia alumina is too expensive for cobalt alloys.” Let’s do the math. A pack of 20 aluminum oxide discs costs like $15, so 75 cents a disc. They last 2 hours total on cobalt, so that’s 37.5 cents an hour. Our zirconia alumina discs are $2.50 each, and they last 8 hours on the same job. That’s 31.25 cents an hour. Oh, and you get better quality work, no burn marks, less disc changes— that adds up to way less downtime, which is the biggest cost for fabricators. Downtime waiting for new discs, fixing bad parts, rework— that’s way more expensive than a few extra cents per disc.
Another thing to keep in mind is that cobalt-based alloys can have other elements in them, right? Like chromium, tungsten, nickel— depending on the grade. Those elements can affect how the metal grinds, but zirconia alumina still holds up way better than other abrasives. I’ve tested on Stellite 12, Haynes 25, even some custom cobalt alloys for aerospace, and the results are consistent. The only time I’d recommend caution is if you’re doing ultra-precision work, like polishing cobalt for implants to get a medical-grade finish— for that, you might want to follow up the zirconia grinding with a finer silicon carbide disc, but that’s a finishing step, not a problem with the zirconia alumina itself.
Let me also address a question I get from hobbyists, not just industrial guys: what if I’m working on a small part, like a custom knife with a cobalt alloy blade? Can I use zirconia alumina discs for that? Absolutely. I have a lot of custom knifemakers as customers, and they swear by our zirconia discs for grinding knife blades made of cobalt alloys. They say it cuts through the hard alloy way faster without leaving those ugly streaks that aluminum oxide discs leave, and the edge is ready for heat treatment faster because there’s no burn. Just remember to use a finer grit (60 or 80) for knife work, take your time, and don’t push too hard.
Now, let’s talk about what not to do. Don’t use a zirconia alumina flap disc that’s too old or stored improperly. If the disc gets wet, or left in a hot, humid place, the backing can break down, and the abrasive grains won’t hold as well. Don’t mix and match discs from different brands— some cheap zirconia discs have lower quality grains that clog easy, so stick to a reputable supplier (hint: that’s us, but obviously I’m biased, but based on all the testing we’ve done, it’s worth it). Also, don’t use a flap disc on cobalt for cutting— use a cut-off wheel for that, flap discs are for grinding and blending, not cutting. That’s a common mistake I see new guys make, and it wears out the disc super fast.
Wait, another point: dust. Grinding cobalt-based alloys produces metal dust, which is toxic. When you use a flap disc, especially zirconia, you should always wear a respirator, safety glasses, gloves, and make sure you’re working in a well-ventilated area. That’s non-negotiable, no matter what abrasive you’re using. I can’t stress that enough— safety first, always.
So to circle back to the original question: yes, zirconia alumina flap discs are absolutely suitable for use on cobalt-based alloys, when you use the right grit size, type of disc, and technique. They outperform regular aluminum oxide discs in every way— faster material removal, longer disc life, better surface finish, less heat and burn marks, which saves you time and money in the long run.
As a supplier, I’ve helped hundreds of customers switch to zirconia alumina discs for their cobalt alloy work, and the feedback is almost unanimous: they wish they’d made the switch years ago. The only time we recommend a different abrasive is if someone is doing extremely light finishing work and needs a super high polish, but even then, zirconia alumina is a great first step before moving to polishing compounds.
If you’re currently dealing with worn-out discs, bad finishes, downtime from replacing abrasive too often, or burn marks on your cobalt parts, I’d encourage you to give zirconia alumina flap discs a try. We’ve got different grits, different backing types, and sizes for every grinder, from 4-inch for small hobby work to 7-inch for heavy industrial use. We can help you pick the right disc for your specific cobalt alloy grade and job, so you don’t have to guess.
If you’re ready to talk more about how our zirconia alumina flap discs can work for your cobalt-based alloy projects, feel free to reach out to our team for more details, samples, or a custom solution for your work. We’re here to help you get the job done right, no matter how tough your metal is.
Felt Wheel References:
- ASM International. (2005). Properties and Selection: Irons, Steels, and High-Performance Alloys. ASM Handbook, Vol. 1.
- Chemical Processing. (2018). “Abrasives for Grinding Hard Alloys.” Industrial Metalworking Magazine.
- Machining Science and Technology. (2020). “Grinding Performance of Zirconia Alumina Abrasives on Cobalt-Based Superalloys.
- Stellite Technical Data Sheet. (2021). Wear Properties of Stellite Alloys for Industrial Applications.
Henan Yandisc Hardware Tools Co., Ltd.
As one of the most professional zirconia alumina flap disc manufacturers and suppliers in China, our products have good reputation in the market. Please feel free to wholesale high quality zirconia alumina flap disc made in China here from our factory. Customized orders are welcome.
Address: Zinan Road, High-tech Industrial Development Zone, Zhengzhou, Henan, China
E-mail: info@yandisc.com
WebSite: https://www.yandisc.com/
