Alright, let’s talk about something not so glamorous but super important if you’re running an EPS molding operation—cleaning your EPS shape molding machine. I know, I know, when you’re cranking out custom packaging, insulation, or those fun foam toys, the last thing you want to do is tear apart your machine for a deep clean. But here’s the thing: skip this step, and you’ll end up with lousy part quality, clogged nozzles, higher energy bills, and parts that just don’t fit right. As someone who’s been supplying EPS molding machines for years, I’ve seen way too many clients cut corners on cleaning and regret it later. So let’s break this down like we’re chatting over a coffee, no super technical jargon (I’ll keep it real, promise). EPS Shape Molding Machine
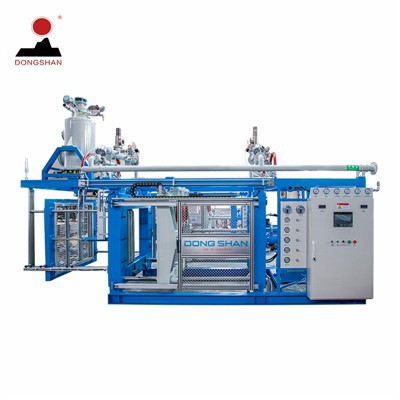
First, let’s get one thing straight: cleaning isn’t a one-size-fits-all job. How often you do it depends on how much you run your machine, the type of EPS beads you use (virgin vs. recycled, because recycled stuff is way stickier), and the parts you’re making. If you’re running 24/7 with recycled EPS, you’ll need a quick daily wipe-down and a full deep clean every 2 weeks. If you’re on a slower schedule with virgin beads, a monthly deep clean is probably enough. The last mistake I see folks make is waiting until their machine is totally caked with old foam—by then, you’re looking at hours of scraping and maybe even damaging parts. Let’s start with the daily routine, because staying on top of small messes is way easier than fixing big ones.
Daily cleaning takes 10–15 minutes max, I swear. As soon as you finish your last run of the day (and before you shut off the machine for good), grab a soft, lint-free cloth (microfiber works best, no rough paper towels—those leave scratches or bits of lint that can get into your next batch of parts) and a tiny bit of warm water. No harsh chemicals here—EPS is made of polystyrene, and chemicals like bleach or heavy degreasers can break down the machine’s rubber seals or even the interior of the mold. First, wipe down the exterior parts: the control panel (don’t spray water directly on it—damp cloth only!), the clamping arms, the steam lines on the mold, and the hopper where you load the EPS beads. Wait, the hopper? Yeah, that’s a hot spot. If old beads are left in there, they’ll start to pre-expand a little and get sticky, so dump any leftover beads into a sealed container (you can still use them if they’re not degraded) and wipe the hopper walls clean. Next, the nozzle—super important because clogged nozzles = no parts coming out right. The nozzle is where the EPS beads get injected, so use that same damp cloth to swab it out gently. If there’s a tiny bit of dried foam, a wooden skewer (not metal—metal can scratch the nozzle tip!) works to nudge it loose. Just be careful not to bend or chip the nozzle. Finally, double-check the drain on the machine—sometimes condensed water or leftover foam bits collect there, so a quick swish with warm water keeps it from getting clogged. That’s it for daily stuff—easy peasy.
Now, the deep clean. This is the one that makes most people groan, but trust me, it’s non-negotiable. I recommend doing a full deep clean every 200–300 production cycles, or whenever you switch bead types (like from fine beads to coarse, or virgin to recycled). Let’s walk through this step-by-step, like we’re doing it together. First, unplug the machine and let everything cool down completely. I can’t tell you how many times someone tries to take apart a hot mold and gets burned—don’t be that person. Give it at least 2 hours, maybe more if you run it a lot. While you wait, gather your supplies: lint-free cloths, wooden skewers, warm soapy water (mild dish soap is fine, nothing heavy), a soft-bristled brush (toothbrush works great for small crevices), and a bucket. No pressure washers, no high-pressure air—those can blow bits of foam into places you can’t reach and damage delicate parts like the mold’s inner cavities.
Once everything is cool, start with the mold—this is where 90% of the gunk builds up. The mold is the metal part that gives EPS its shape, right? You’ll need to unclamp it (follow your machine’s specific steps, every model is a little different) and separate the two halves. Dump any loose bead residue into your bucket, then take your soft brush and warm soapy water and gently scrub every inch of the mold’s inner cavities and the steam holes. Those tiny steam holes are the worst—clogged ones mean uneven heating, which means warped parts. Use the wooden skewer to clear out any stuff stuck in the steam holes, just be gentle so you don’t widen them. If there’s really stubborn, dried foam, let the mold soak in warm soapy water for 15 minutes first—this softens it so it wipes right off. Don’t use a scraper on the mold unless it’s a plastic or rubber one—metal scrapers will scratch the surface, and scratches will show up on your parts (not good for custom orders that need a perfect finish).
Next up, the steam lines. These carry the steam that expands the EPS beads, so if they’re clogged with old foam, steam can’t get through evenly. First, disconnect the steam lines from the machine and the mold (again, make sure they’re totally cool—steam lines hold heat for ages). Hold them over your bucket and pour warm soapy water through them, then gently push a wooden skewer through each line to clear out any blockage. You’ll be surprised how much gunk comes out—this is why even if your parts look fine, the inside of the lines are getting dirty. Once they’re clear, rinse them with clean water and let them air dry completely before putting them back—any leftover water will mix with steam next time and cause wet, soggy parts.
Then there’s the hopper and the feed system. Dump any remaining beads from the hopper, then remove the hopper if your machine lets you (most are easy to take off with a few screws). Wipe it down with soapy water, then rinse and dry. For the feed system—the part that moves beads from the hopper to the nozzle—use your soft brush to get into all the nooks. If there’s a lot of built-up gunk, you can use a tiny bit of isopropyl alcohol on a cloth (just a little, don’t douse it) to dissolve the foam, then wipe it dry right away. Alcohol evaporates fast, so no water spots or leftover moisture.
Wait, what about the machine’s interior? The part under the mold where the clamping happens? You can wipe that down with a damp cloth, but be careful not to get water on the electrical components (they’re usually sealed, but better safe than sorry). If there’s a lot of foam dust there, a small vacuum with a soft brush attachment works, but don’t suck up any loose metal bits or you’ll damage the vacuum (or the machine!).
Once you’ve got all the parts cleaned, it’s time to put everything back together—but don’t just snap it all together. Let’s do a quick check. Make sure the mold is aligned correctly (misalignment leads to parts that don’t close right) and all the steam holes are still clear. Test the nozzle by blowing through it gently (use your mouth, or a tiny air compressor set to low pressure) to make sure nothing’s stuck. If you’re switching bead types, now’s a good time to run a small “purging cycle” with a little virgin EPS beads—this clears out any leftover gunk from the feed system before you start your next production run. Run a test part first, just to make sure everything is working right—no weird warps, no uneven edges, no clogs.
Here’s a pro tip I only share with my regular clients: don’t forget the seals. The rubber seals around the mold and the hopper get worn and dirty over time, and if they’re not cleaned, they can leak steam or beads, which messes up part quality. Wipe them down with a damp cloth every clean, and if they’re cracked or super sticky, replace them—they’re cheap, and saving them will save you hours of fixing bad parts later.
Another thing: avoid common mistakes. I see people use too much water on the control panel all the time—this leads to electrical issues, which is a nightmare. Or they use harsh chemicals that eat away at the mold’s coating, so parts start to stick. Or they skip the deep clean and wonder why their machine is breaking down faster than it should. Cleaning your EPS molding machine isn’t just maintenance—it’s extending its lifespan. A client of mine bought a used machine 5 years ago, and even though it was a little beat up, they stuck to a strict cleaning routine and it’s still running like a top. The machines I sell come with a quick-start cleaning guide, but I always tell them this blog-style tips are the real game-changer.
If you’re new to running an EPS molding machine, or you’re having trouble getting consistent part quality, maybe your cleaning routine is slipping. Even if you’re in the middle of a big order, carve out that 10 minutes for daily cleaning. It pays off in fewer rejects, less downtime, and a machine that lasts way longer than it would if you skip this step.
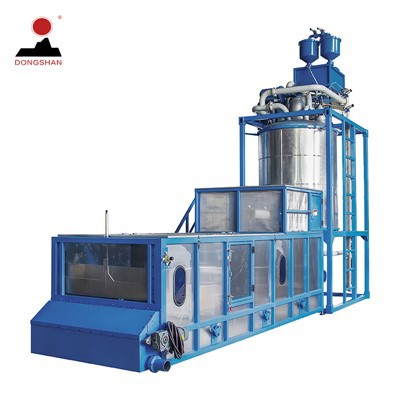
If you’re in the market for a new EPS shape molding machine, or you need replacement parts for your current one, feel free to reach out to connect for a chat. We know how busy your production schedule is, so we don’t push hard sells—we just want to make sure you’ve got the right equipment and tips to keep your line running smoothly.
EPS Cutting Machine References:
- Society of the Plastics Industry. (2021). EPS Molding Equipment Maintenance Best Practices.
- Foam Packaging Association. (2022). Guide to Cleaning and Maintaining EPS Shape Molding Machinery.
- International Journal of Manufacturing Technology and Management. (2020). Effects of Cleaning Schedules on EPS Molding Part Quality.
Hangzhou Fuyang Dongshan Plastic Machinery Co., Ltd.
Hangzhou Fuyang Dongshan Plastic Machinery Co., Ltd. is one of the most professional EPS shape molding machine manufacturers and suppliers in China, featured by quality products and low price. Please feel free to wholesale advanced EPS shape molding machine made in China here and get quotation from our factory. Customized orders are welcome.
Address: 101 Guanting, Baiqian Villige, Luzhu Town, Fuyang District, Hangzhou City, Zhejiang Province, China
E-mail: xu@dong-shan.cn
WebSite: https://www.epseppmachinery.com/
